NJ & NYC Commercial & Residential Garage Door
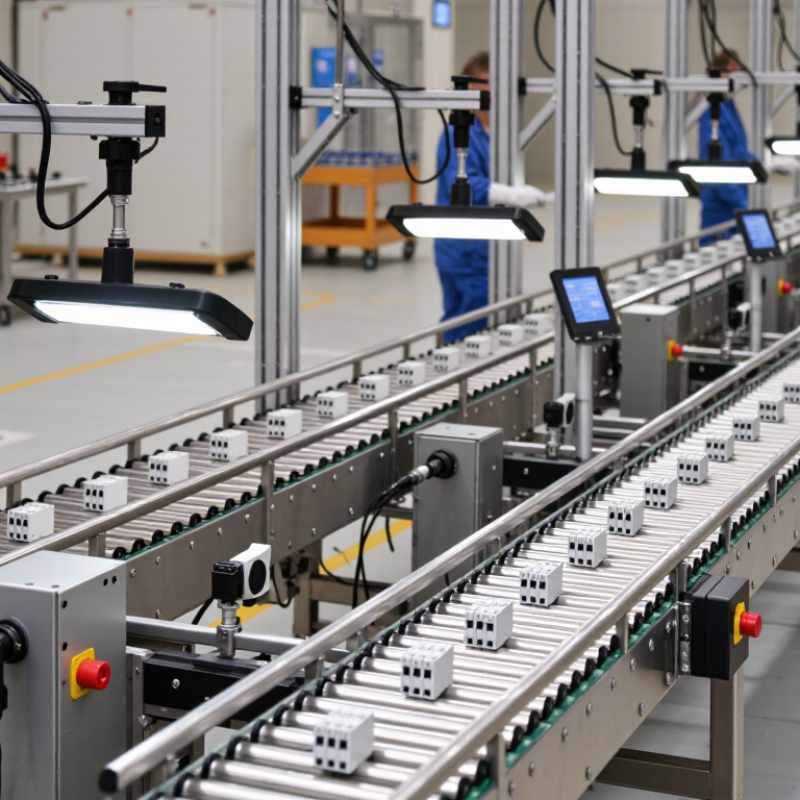
A Mcb Inspection Conveyor is a specialized system for checking miniature circuit breakers during production. It moves each breaker through controlled inspection points without unnecessary manual handling. Operators can examine housing condition, label placement, terminal alignment, and visible assembly defects. The conveyor also supports testing equipment, barcode readers, cameras, and reject mechanisms.
In a well-designed line, speed should never replace accuracy. Each station needs stable positioning, suitable lighting, and clearly defined inspection criteria. A practical system may use adjustable guides to prevent breakers from tilting as they travel. Small details matter. A loose sensor bracket can create repeated false readings. Poor spacing can also cause two products to enter one inspection zone.
From my experience with industrial inspection equipment, the conveyor is only one part of quality control. Reliable results depend on calibration, maintenance, operator training, and complete production records. Engineers should consider product dimensions, line capacity, electrical safety, cleaning requirements, and future upgrades before selecting a configuration. It is tempting to focus on speed, but that approach can hide weak inspection logic. A slower, traceable process may deliver better results.
This guide explains how a Mcb Inspection Conveyor works, which components it includes, and where it fits within modern manufacturing. It also discusses common design choices, operational limitations, and maintenance practices. Some applications require customization. No single conveyor suits every factory. Performance should be verified with real products, measured data, and documented trials. That evidence makes the final system more dependable.
What Is an MCB Inspection Conveyor?
Definition and Purpose of an MCB Inspection Conveyor
An MCB inspection conveyor is a controlled transport system for miniature circuit breakers. It moves each unit through inspection and testing stations at a steady rate. The conveyor may carry breakers in trays, fixtures, or individual pockets. This arrangement reduces manual handling and keeps product orientation consistent.
Its main purpose is to support reliable quality checks. Cameras can inspect housing condition, labels, terminal position, and toggle alignment. Sensors may confirm presence, dimensions, and correct assembly. Electrical stations can test continuity or operating performance when the production design requires it. A reject mechanism then separates questionable units from approved products. That matters.
In practical production, stable movement is as important as the inspection device itself. Uneven spacing can cause missed images or false results. Dust, vibration, and worn fixtures may also affect accuracy. Regular cleaning, calibration, and fixture checks help control these risks. Operators should review inspection records and investigate repeated failures instead of simply removing them. A conveyor cannot repair poor process settings. It only reveals them.
The system should include guarding, emergency stops, clear status signals, and documented maintenance procedures. Inspection data can support traceability when linked to time, batch, and station information. However, automation is not infallible. A well-designed line still needs trained personnel to question unusual patterns and verify borderline results.
An MCB inspection conveyor moves miniature circuit breakers through controlled inspection stations. Its core components include an infeed belt, product fixtures, guide rails, sensors, test units, and an outfeed conveyor. Each part must maintain stable spacing. Small positioning errors can affect test results.
The operating principle is straightforward. The infeed belt delivers MCBs to a timing section. Sensors detect each unit and confirm its position. A servo-driven indexing mechanism then moves products into fixed inspection zones. There, cameras check housing condition, terminal alignment, markings, and assembly details. Electrical stations may verify continuity, insulation resistance, or trip performance under controlled conditions. A PLC coordinates movement, timing, test signals, and rejection commands.
Accuracy depends on more than software. Clean guide rails, steady belt tension, and correctly adjusted fixtures matter every shift. I have found that dust near sensors can create false rejects. That issue is easy to overlook. A pneumatic or mechanical reject unit separates failed products from accepted ones. The conveyor should also stop when a guard opens or a sensor detects a blockage. Operators need clear access for calibration and maintenance. No inspection line is perfect. Product variation, vibration, and worn fixtures still require regular review. Recording inspection data helps technicians trace recurring faults and improve settings over time.
An MCB inspection conveyor is more than a moving belt. It coordinates controlled checks for miniature circuit breakers as they travel between stations. Each carrier keeps one device aligned, reducing handling errors and protecting test results. In production, technicians watch spacing, sensor timing, and reject signals. Small faults matter. A tilted breaker can distort a camera reading or damage a test probe.
The inspection stages usually begin with presence and orientation checks. Cameras confirm the housing, toggle position, markings, and visible cracks. Dimensional gauges then verify critical profiles, terminal locations, and assembly height. Next, electrical stations may measure continuity, insulation resistance, and operating behavior. Trip testing requires controlled current and calibrated instruments. Safety interlocks should stop the conveyor when a guard opens or a device sits incorrectly. These controls support repeatable testing, but settings must match the approved technical specification.
A final station reviews labels, terminal condition, and overall cleanliness. The system separates accepted units from suspect ones and records results by batch or serial reference. That record supports maintenance, investigations, and customer confidence. Experienced teams also inspect the conveyor itself. They check probe wear, belt tracking, sensor lenses, and calibration status. No line is perfect. A camera may miss a shallow defect, while a worn probe can create a false failure. Manual review remains valuable for unusual results. I would question any process reporting zero defects every day. Stable production is possible, but measurement systems still need challenge samples, independent checks, and periodic review.
An MCB inspection conveyor moves miniature circuit breakers through controlled inspection stations. It maintains stable spacing, lighting, and camera positions. In production audits, consistency matters more than speed alone. Each carrier should hold the device firmly without hiding terminals or the toggle. Conveyor vibration must remain low. Otherwise, images may blur and electrical tests may become unreliable. The system often combines visual inspection, dimensional checks, and functional testing.
Important quality parameters include housing cracks, flash, discoloration, terminal alignment, screw presence, label readability, and toggle position. Inspectors also verify width, height, mounting features, and contact spacing against approved drawings. Camera exposure needs routine checks. Reflections can resemble cracks. Weak lighting may conceal shallow marks. Force and travel limits should be recorded during mechanical tests. Electrical checks may confirm insulation resistance, continuity, and trip behavior under validated conditions. Tolerances must follow controlled specifications, not operator preference.
Defect detection commonly uses industrial cameras, edge analysis, presence sensors, and calibrated gauges. Vision software can identify missing parts, uneven surfaces, wrong positions, and damaged housings. A reject signal then separates suspicious units from accepted products. However, automation is not infallible. Dust, glare, and slight carrier movement can create false alarms. A trained inspector should review unclear images and monitor defect trends. No inspection method is flawless. Sampling plans also deserve regular review, because a low defect rate does not always prove complete process control.
Quality parameters and defect detection methods for miniature circuit breakers (MCBs), including visual inspection, dimensional checks, terminal verification, contact testing, and trip-function testing.
The conveyor camera checks housing damage, missing labels, lever position, terminal presence, and assembly alignment before electrical testing.
Continuity, insulation resistance, and pole-to-pole contact measurements help identify open circuits, short circuits, and poor internal connections.
Current injection verifies that the breaker trips within the time limits defined by the applicable product specification and safety standard.
The chart shows representative inspection checkpoints and their relative contribution to automated defect detection. Actual acceptance limits should be configured according to the MCB design, rated current, applicable standard, and validated production-control plan.
An MCB inspection conveyor moves miniature circuit breakers through controlled inspection points. It supports safety checks, maintenance routines, and steady production flow. Operators can examine terminal alignment, housing damage, label placement, and switching movement without handling every unit manually. In a working line, guarded transfer sections reduce contact with moving parts. Emergency stops should remain visible and accessible. Sensors must detect jams before products pile up. A conveyor is not automatically safe, though. Poor lighting, loose wiring, or rushed adjustments can create serious risks.
Tips: Clean guide rails daily. Check belts for cracks and uneven tension. Test emergency stops before each shift. Record sensor faults, even when production continues. Small faults rarely stay small.
Maintenance teams should inspect bearings, rollers, fasteners, and electrical connections at planned intervals. Dust around sensors may cause missed inspections. Excessive vibration can signal misalignment or worn components. Production staff should also confirm that conveyor speed matches the inspection process. Faster is not always better. A slower, stable line may prevent rejected units and operator fatigue. Inspection results should be traceable through dated records, sample checks, and clear acceptance criteria. These details support reliable decisions and help engineers identify repeated failures. Still, manual review remains valuable because automated systems can miss unusual damage, especially when product variations are not included in the inspection setup.
| Data Dimension | Typical Information | Inspection or Production Relevance |
|---|---|---|
| Equipment Definition | A motor-driven conveyor system that transfers miniature circuit breakers (MCBs) between assembly, inspection, testing, marking, and packaging stations. | Provides controlled product movement and repeatable positioning for automated or semi-automated quality checks. |
| Products Handled | Single-pole, double-pole, triple-pole, and four-pole MCB assemblies, depending on the conveyor fixture and product family. | Changeover tooling may be required for different product widths, pole counts, terminal layouts, or housing dimensions. |
| Common Conveyor Type | Belt, chain, timing-belt, or palletized conveyor with dedicated nests or fixtures. | Palletized and fixture-based systems generally provide better orientation control for vision and electrical test stations. |
| Typical Conveyor Speed | Approximately 5–20 m/min for inspection lines; the final value depends on product size, station cycle time, and required test duration. | Speed must be synchronized with inspection exposure time, actuator response, and safe access requirements. |
| Positioning Accuracy | Typically designed within approximately ±0.5–1.0 mm at a dedicated inspection position, subject to fixture and sensor design. | Consistent positioning improves camera focus, terminal probing, actuator alignment, and repeatability of test results. |
| Product Orientation | The MCB is normally presented with a defined top, front, terminal, and handle orientation using guide rails, nests, or locating pins. | Prevents incorrect images, probe contact errors, reversed products, and missed visual defects. |
| Visual Inspection Points | Housing damage, cracks, flash, color variation, missing components, incorrect markings, handle position, terminal condition, and assembly completeness. | Camera inspection reduces dependence on manual visual checks and creates traceable pass/fail records. |
| Dimensional Inspection | Overall length, width, height, terminal spacing, mounting features, and critical assembly positions are checked against approved product drawings. | Confirms that the MCB can be installed correctly and remains compatible with its intended mounting system. |
| Electrical Inspection | Depending on the product specification, checks may include continuity, dielectric withstand, insulation resistance, contact resistance, and trip-function testing. | Electrical test parameters must be controlled according to the applicable product standard, approved test procedure, and rated design. |
| MCB Protection Functions | MCBs commonly use thermal protection for prolonged overcurrent and magnetic protection for high-current short-circuit conditions. | Inspection and testing help verify assembly quality, mechanism operation, and conformity with the specified trip characteristics. |
| Handle and Mechanism Check | The operating handle, toggle position, latch mechanism, and visual ON/OFF/TRIP indication are checked for correct movement and position. | Detects incomplete assembly, mechanical interference, incorrect indication, or excessive operating resistance. |
| Safety Guarding | Fixed guards, interlocked access doors, emergency-stop devices, electrical enclosures, and clearly identified hazardous zones. | Protects operators from moving parts, electrical test hazards, pinch points, and unexpected machine start-up. |
| Electrical Safety Controls | Protective earthing, overcurrent protection, residual-energy control, guarded test probes, and lockout/tagout procedures. | Electrical testing should be performed only with suitable safeguards, trained personnel, and verified test equipment. |
| Reject Handling | Rejects may be diverted into a locked or clearly identified bin using a pneumatic stop, servo actuator, or controlled chute. | Separates nonconforming products from accepted products and supports later root-cause analysis. |
| Traceability Data | Typical records include product type, lot or serial identifier, station result, test value, timestamp, operator or line ID, and reject reason. | Enables defect investigation, process capability monitoring, audit support, and controlled product release. |
| Throughput Calculation | Theoretical output is approximately 3,600 ÷ cycle time in seconds per product; practical output is lower because of stops, changeovers, rejects, and maintenance. | Station cycle time, conveyor pitch, and buffer capacity should be balanced to avoid bottlenecks. |
| Daily Maintenance | Remove dust and plastic debris, inspect guards and sensors, verify emergency stops, check product nests, and observe abnormal noise or vibration. | Routine checks reduce misfeeds, sensor faults, contamination-related defects, and unplanned downtime. |
| Periodic Maintenance | Inspect belt or chain tension, alignment, bearings, fasteners, drive components, pneumatic connections, cables, and calibration status. | Maintenance intervals should follow equipment condition, operating hours, manufacturer instructions, and site risk assessments. |
| Common Failure Modes | Product jams, belt tracking errors, sensor misalignment, fixture wear, camera contamination, probe wear, communication faults, and actuator failure. | Fault codes, inspection logs, and downtime records help identify recurring problems and prioritize corrective action. |
| Production Applications | Assembly-line transfer, in-process inspection, end-of-line testing, automatic marking, sorting, packing, and controlled buffer storage. | The conveyor connects separate operations into a repeatable production flow while reducing manual handling. |
| Key Performance Indicators | Throughput, first-pass yield, reject rate, false-reject rate, unplanned downtime, mean time between failures, and mean time to repair. | These indicators show whether the conveyor is improving quality, availability, and production consistency. |
| Design Consideration | Conveyor layout should provide adequate access, clear product flow, ergonomic loading, safe maintenance space, and suitable electrical-test separation. | A balanced design improves operator safety, inspection reliability, maintenance efficiency, and overall equipment effectiveness. |
Note: Conveyor dimensions, speeds, tolerances, and electrical test settings are typical engineering references. Final values must be verified against the approved product drawings, applicable safety requirements, and the specific inspection-system design.