NJ & NYC Commercial & Residential Garage Door
China Top 10 Conveyor Equipment Manufacturers
China’s conveyor manufacturing sector has grown from basic belt systems into a broad industrial supply network. Today, buyers can find solutions for mining, logistics, ports, food processing, warehouses, and automated factories. This article introduces China’s top 10 conveyor equipment manufacturers and examines what makes each company worth attention.
The review considers product range, engineering experience, production capacity, quality control, customization, and after-sales support. It also looks at practical details, such as belt width, frame materials, motor efficiency, load capacity, and delivery requirements. A reliable supplier should provide clear drawings, testing records, installation guidance, and responsive technical communication. Factory visits, sample inspections, and reference projects can reveal more than attractive catalog images. Small details matter.
No ranking is permanently correct. Market performance, export experience, pricing, and technology can change each year. Some manufacturers may excel in heavy-duty conveyors, while others focus on modular systems or warehouse automation. A supplier with impressive machinery may still have weak overseas service. That point deserves reflection. Buyers should verify certifications, component brands, warranty terms, and spare-parts availability before signing contracts. The phrase “Conveyors Equipment” is often used broadly, but actual performance depends on correct system design and operating conditions. This guide aims to offer a balanced starting point, not a substitute for technical evaluation. It combines industry-focused criteria with practical observations, helping readers compare manufacturers more carefully and select equipment that fits their material, space, safety, and maintenance requirements.
Definition and Scope of Conveyor Equipment Manufacturing in China
China Top 10 Conveyor Equipment Manufacturers
Definition and Scope of Conveyor Equipment Manufacturing in China
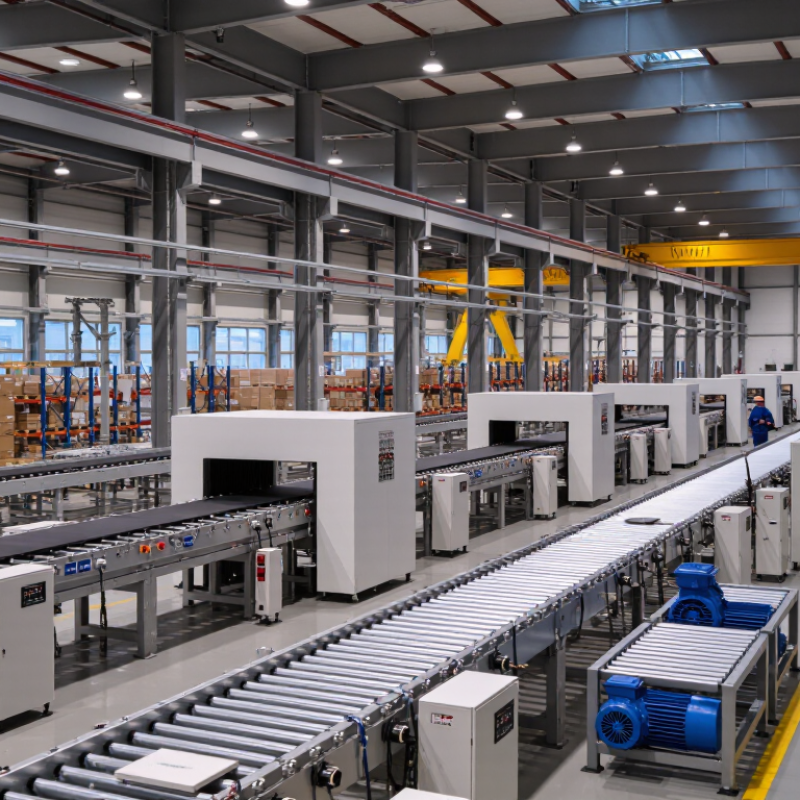
Conveyor equipment manufacturing in China covers machines that move bulk or unit loads through controlled routes. The scope includes belt, roller, chain, screw, bucket, pipe, and vibrating conveyors. It also covers frames, pulleys, drives, sensors, controls, loading stations, and safety guards. These details matter. A conveyor is rarely a single machine.
Chinese manufacturers serve mining, ports, warehousing, logistics, food processing, cement, and automobile production. The National Bureau of Statistics reported that China’s equipment manufacturing value added grew 7.7% in 2024. This figure does not isolate conveyors, but it reflects strong demand for industrial equipment. Grand View Research also identifies Asia-Pacific as the leading regional market for conveyor systems, supported by factory automation and warehouse expansion.
In practice, classification can be difficult. A complete conveyor line may include electrical control cabinets, software, structural steel, and installation services. Some suppliers manufacture core equipment, while others integrate purchased components. That boundary is not always clean. The China Statistical Yearbook groups many products under broader machinery categories, limiting direct market comparisons. Buyers should therefore check product drawings, load capacity, speed, belt width, operating temperature, and compliance records. ISO 5048 offers calculation guidance for belt conveyor power and capacity, while national standards may define additional safety requirements. A supplier’s catalogue is useful, but independently verified test data is stronger.
| No. | Equipment Category | Definition and Typical Configuration | Main Conveyed Materials | Typical Industries | Key Manufacturing Scope | Relevant Technical Reference |
|---|---|---|---|---|---|---|
| 1 | Belt Conveyors | Continuous conveyors using an endless belt supported by idlers or a slider bed. Configurations may include troughed, flat, inclined, reversible, and enclosed designs. | Coal, ore, aggregates, cement, grain, parcels, and packaged goods | Mining, ports, power generation, cement, logistics, and agriculture | Structural frames, pulleys, idlers, drive units, belts, transfer chutes, guarding, and dust-control systems | ISO 5048; ISO 14890; relevant machinery-safety requirements |
| 2 | Bucket Elevators | Vertical lifting equipment that uses buckets attached to a belt or chain to move bulk materials upward. | Grain, flour, fertilizer, cement, minerals, and dry powders | Agriculture, food processing, fertilizer, cement, and chemical processing | Head and boot sections, buckets, belts or chains, casing, tensioning devices, inspection doors, and discharge systems | EN 618; ISO 12100; application-specific explosion-protection requirements where applicable |
| 3 | Screw Conveyors | Enclosed or open conveyors that move bulk materials through a rotating helical screw flight inside a trough or tube. | Powders, granules, sludge, ash, feed, and food ingredients | Food, chemical, wastewater, agriculture, cement, and environmental services | Flighting, troughs or tubes, shafts, bearings, gear drives, inlet and outlet sections, liners, and sealing systems | ANSI/CEMA 350; ISO 12100; hygienic-design requirements for food applications |
| 4 | Drag Chain Conveyors | Heavy-duty enclosed conveyors using one or more chains with flights or attachments to move bulk material horizontally or on an incline. | Coal, ash, clinker, biomass, wood chips, and bulk minerals | Power generation, cement, mining, biomass, and material handling | Chains, flights, drive sprockets, casings, wear liners, tensioning systems, and discharge arrangements | ISO 12100; chain and machinery-safety specifications applicable to the system design |
| 5 | Apron Conveyors | Conveyors formed from overlapping metal or reinforced pans attached to chains, designed for severe impact and high-temperature service. | Ore, limestone, clinker, slag, rock, and hot bulk solids | Mining, metallurgy, cement, foundries, and heavy industry | Apron pans, chains, sprockets, rollers, drive assemblies, impact beds, skirts, and heavy-duty support structures | ISO 12100; ISO 1977 for conveyor chain-related design considerations |
| 6 | Roller Conveyors | Material-handling systems using powered or gravity rollers to transport pallets, cartons, totes, and rigid-bottom loads. | Cartons, pallets, containers, bins, and assembled products | Warehousing, e-commerce, manufacturing, parcel handling, and distribution | Rollers, frames, motors, drive belts or chains, sensors, accumulation zones, transfers, and control interfaces | EN 619; ISO 12100; warehouse and automated-material-handling safety practices |
| 7 | Slat and Chain Conveyors | Conveyors using metal or engineered-plastic slats driven by chains for stable transport, accumulation, or indexing of discrete products. | Bottles, cans, containers, cartons, and packaged consumer goods | Food and beverage, packaging, pharmaceuticals, and consumer products | Slats, chains, sprockets, wear strips, guide rails, frames, lubrication systems, and washdown-compatible components | EN 619; ISO 14159 for hygienic design where applicable |
| 8 | Pneumatic Conveyors | Systems that transport powders or granular materials through pipelines using air pressure or vacuum. | Powders, pellets, granules, flour, resin, and pharmaceutical ingredients | Chemical, food, plastics, pharmaceuticals, and battery-material processing | Blowers or vacuum pumps, pipelines, rotary valves, filters, separators, feeders, instrumentation, and control systems | ISO 12100; ATEX or equivalent hazardous-area requirements where applicable |
| 9 | Overhead Conveyors | Elevated trolley, chain, or power-and-free systems that transport products above the floor and may include accumulation or routing functions. | Hanging parts, garments, automotive components, boxes, and containers | Automotive, surface finishing, garment manufacturing, warehousing, and assembly | Tracks, trolleys, chains, drives, switches, carriers, load hangers, accumulation devices, and safety guarding | EN 619; ISO 12100; application-specific lifting and workplace-safety requirements |
| 10 | Mobile and Telescopic Conveyors | Portable, radial, shuttle, or telescopic conveyor systems designed for flexible loading, unloading, stockpiling, or truck and container handling. | Bulk solids, parcels, cartons, baggage, and palletized goods | Ports, warehouses, logistics, mining, agriculture, and construction materials | Mobile chassis, telescopic sections, hydraulic or electric actuation, belt assemblies, wheels, controls, and stabilization systems | ISO 12100; EN 60204-1 for electrical equipment; relevant mobile-equipment safety requirements |